The short answer
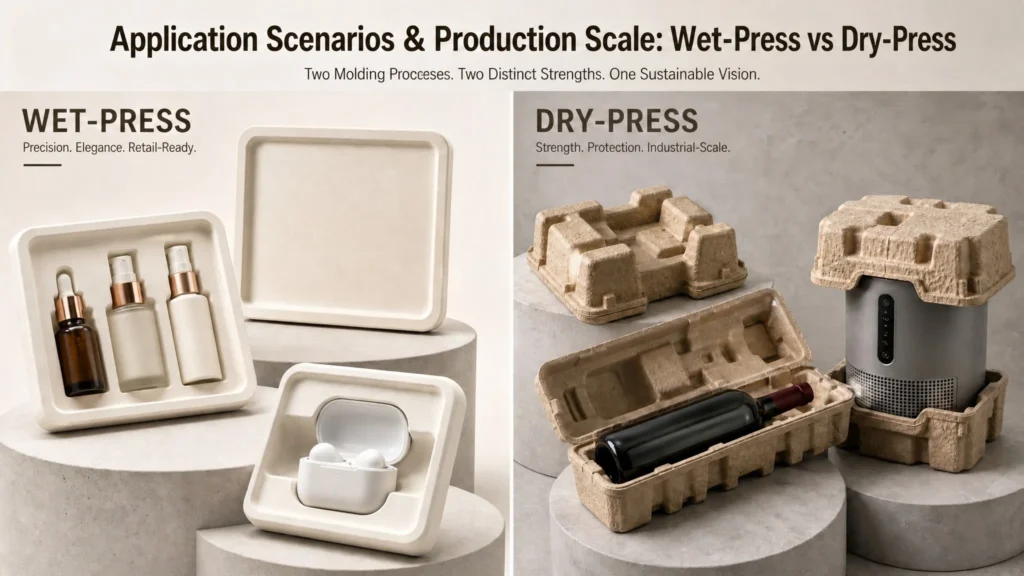
- Wet-press: wall thickness 0.8–1.5 mm, smooth dense surface, MOQ 1,000 pcs.
- Dry-press: wall thickness 1–3 mm, rougher cushioning surface, MOQ 5,000 pcs.
- Cavity machining tolerance: wet-press ±0.03–0.05 mm in normal production, ±0.02 mm at high precision (down to ±0.015 mm at the limit).
- Dry-press cavity tolerance: ±0.08–0.15 mm in normal production; high precision rarely holds within ±0.05 mm.
- Choose by surface and tolerance requirement, not by unit price — the unit price difference is smaller than the cost of a part that does not fit.
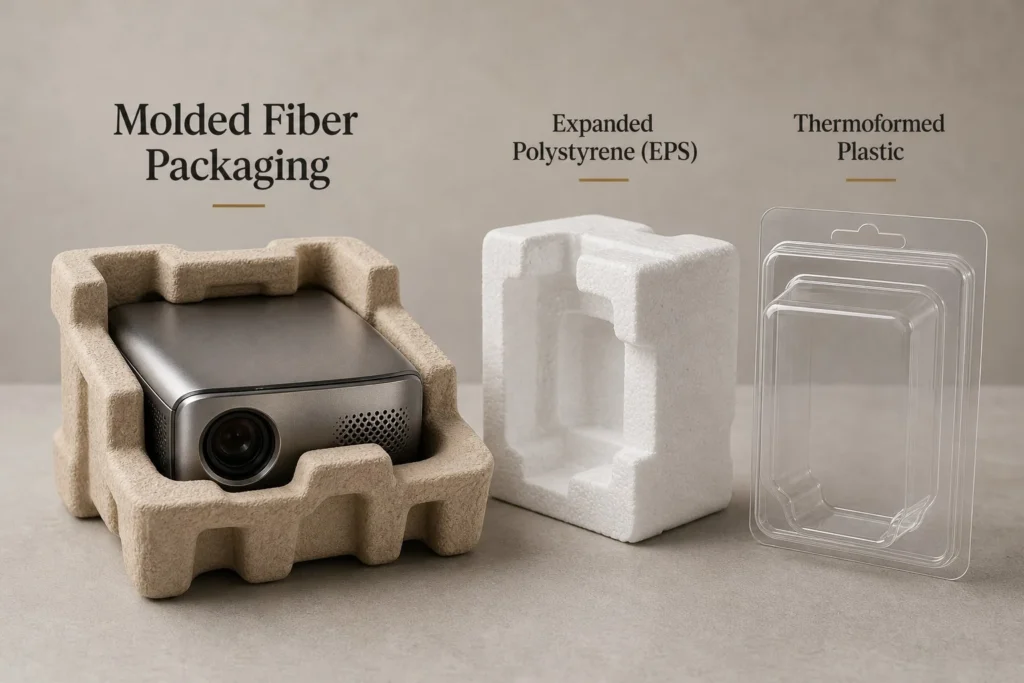
Two molded pulp parts can look similar in a photo and be made by processes that are not interchangeable. The difference shows up in wall thickness, cavity tolerance, surface finish and minimum order quantity. This page compares the two processes we run, with the figures we can hold. For the definition, the fibre grades and the two other process families, see what molded pulp packaging is.
Side-by-side
| Criterion | Wet-press | Dry-press |
|---|---|---|
| Wall thickness | 0.8–1.5 mm | 1–3 mm |
| Cavity machining tolerance | ±0.03–0.05 mm normal ±0.02 mm high precision (limit ±0.015 mm) |
±0.08–0.15 mm normal high precision rarely within ±0.05 mm |
| MOQ per SKU | 1,000 pcs | 5,000 pcs |
| Surface | Smooth, dense, one side finished by the heated tool | Textured, open fibre, visible mesh marks |
| Forming | Pressed between heated matched tools while wet | Formed wet, dried in racks or a tunnel, pressed afterwards |
| Typical products | Cosmetics, electronics, gift boxes, retail inserts | Egg and produce trays, heavy cushioning, industrial corner blocks |
| Printing | Good — smooth surface holds fine print and embossing | Limited — open surface blurs fine detail |
What actually differs in the molded pulp process
Wet-press forms the part from the slurry and presses it between heated matched tools while it is still wet. Water leaves as steam under pressure, so the fibre packs densely and takes the tool surface. That is why it holds thin walls and fine detail.
Dry-press forms the part wet, then dries it in open racks or a tunnel before pressing. Less pressure on a drier part means thicker walls and a more open surface — cheaper per part at volume, but not a retail finish.
The practical consequence: a design drawn for wet-press cannot simply be moved to dry-press to save cost. Wall thickness, draft and rib geometry all have to be redrawn.
Wall thickness in molded pulp: why 0.8–1.5 mm vs 1–3 mm
Thin walls need pressure while the fibre is still wet, which is what the wet-press tool provides. Below about 0.8 mm the wall stops carrying load reliably and the part starts to deform on drying.
Dry-press sits at 1–3 mm because the process relies on material thickness for cushioning rather than on a densely pressed shell. Asking for 1 mm on a dry-press tool is possible on paper but usually fails in the drop test.
Tolerance: read this line carefully
The figures in the table are cavity machining tolerances — the accuracy to which the tool itself is machined. They are not the same as the dimensional tolerance of the finished part.
A finished molded pulp part moves with pulp grade, moisture content and drying shrinkage. Part tolerance is therefore wider than the tool tolerance and is quoted per drawing, per grade. Two suppliers quoting “±0.05 mm” can mean entirely different things: one is talking about the tool, the other about the part. Always ask which.
Where tight part tolerance genuinely matters — a cavity that must locate a connector or a lens — the answer is usually a locating feature in the tool plus a controlled moisture content at packing, not a tighter blanket tolerance on the whole part.
MOQ follows the process
Wet-press starts at 1,000 pcs per SKU. Dry-press starts at 5,000 pcs, because the tooling and drying cycle only amortise at volume. The full cost structure behind these molded pulp floors is on our cost and MOQ page.
Which molded pulp process to choose
- Retail packaging with a visible surface — gift box, cosmetics tray, electronics insert: wet-press. Dry-press will read as industrial.
- Fragile, high-value contents needing precise location — wet-press molded pulp, because the tool holds the cavity geometry.
- High-volume cushioning for produce or eggs — dry-press; thickness is doing the work and nobody sees the surface.
- Pilot runs below 5,000 pcs — wet-press, which is the only route that starts at 1,000.
- Heavy industrial parts needing thick walls — dry-press at 2–3 mm; a wet-press wall that thick wastes material.
Where each process fails in the field
Knowing the typical failure mode matters more than the datasheet, because it tells you which test to insist on before the tool is cut.
- Wet-press, thin wall: deformation and moisture marks after long sea freight. The wall is dense but thin, so it takes up ambient humidity unless the pack is coated or bagged. Ask for the moisture content at packing and test after a humidity cycle, not straight off the line.
- Wet-press, tight cavity: the part fits on day one and binds after a week in a humid warehouse. Cavity geometry has to allow for swelling, not just for the nominal dimension.
- Dry-press, cushioning: the wall crushes progressively under repeated stacking. It is designed to absorb one impact, not to carry a pallet load for six months.
- Dry-press, locating features: open fibre surfaces shed dust and lose edge definition, so a rib on a molded pulp insert that should locate a part may not repeat within the tolerance you drew.
None of these is a reason to avoid a process. Each is a reason to specify the test: a humidity cycle for wet-press, a stacking test for dry-press.
What to put in the RFQ
- Wall thickness you need, and which faces are visible.
- Whether your tolerance figure refers to the tool or the finished part.
- Annual and first-order quantity, so the MOQ floor can be checked.
- Product weight and drop height the pack must survive.
- Whether printing or embossing is required.
- Destination market, if food contact or compostability certification applies.
How to verify the choice was right
Two tests settle most process arguments before production, and neither requires a certification.
- A drop test on the packed retail unit — to ISTA 3A for parcel distribution, or a drop test to ASTM D5276 at the height your route implies. Record which faces were dropped; a single “passed” note is not a result.
- A humidity or stacking cycle — 48 hours in a humid chamber for a wet-press molded pulp part, or a 30-day stacking load for a dry-press cushion. Most field failures appear here, not in the drop test.
Ask the supplier to state what changed between a failed and a passed iteration. That answer tells you whether the process is being engineered or guessed.
Process FAQ
Can dry-press hold ±0.05 mm?
Rarely. Dry-press cavity tolerance sits at ±0.08–0.15 mm in normal production, and high precision seldom holds within ±0.05 mm. If a molded pulp drawing needs tighter than that, the part belongs in wet-press.
Is wet-press more expensive per unit?
Usually yes at the same quantity, because the tool costs more and the cycle is slower. The gap narrows as quantity rises, and it can reverse once you count the cost of a part that fails inspection.
Can I start with wet-press and move to dry-press later?
Only by redrawing. Wall thickness, draft and rib geometry are process-specific, so it is a new tool and a new sample cycle, not a transfer.
Which process is better for food contact?
Both can be supplied in food-grade pulp with an FDA food-contact declaration. The choice is driven by shape and volume, not by food safety.
What is the minimum order for each?
1,000 pcs for wet-press per SKU, 5,000 pcs for dry-press per SKU.
Next step
Send a drawing and tell us which faces are visible plus the drop height the pack must survive. We will tell you which process the part actually belongs in — including when the answer is dry-press and the cheaper quote.
Send a drawing for process selection →
Related: cost, tooling and MOQ explained · certifications and test standards · why brands switch to molded pulp